
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
CNC stands for “computer numerical control” — a system where a computer reads a digital design file and drives a cutting tool along programmed paths, replacing hand-guided routing with precise, repeatable machine movement. In woodworking, the term almost always refers to a CNC router: a motorized spindle mounted on a gantry that carves, cuts, and engraves wood according to coordinates in a file.
When people ask “what does CNC machine mean” or see a part described as “CNC machined,” they’re asking the same thing: the cutting was done by a machine following numeric instructions (coordinates like X12.4, Y8.2) rather than by a person guiding a tool by eye. A “CNC-machined” sign, inlay, or cabinet panel simply means its dimensions came from code, so every copy is identical to within fractions of a millimeter.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


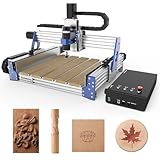
How a CNC Router Actually Works: The CAD-to-Cut Workflow
Every CNC job follows the same four-step pipeline, regardless of machine size:
- CAD (design): You draw the part in design software — VCarve, Easel, Fusion 360, or a vector program. This produces the shapes, not the tool movements.
- CAM (toolpaths): CAM software converts the drawing into toolpaths: which bit, how deep per pass, how fast, and in what direction. The output is G-code, a plain-text list of coordinates and commands.
- Control: A controller (software like GRBL on an Arduino-class board, or a standalone pendant) streams the G-code to stepper motors that move the machine.
- Cutting: The spindle spins the bit — typically 10,000–24,000 RPM for wood — while the machine moves it through the programmed path. Climb vs. conventional milling, feed rate, and depth per pass all come from your CAM settings.
The workflow is the real learning curve, not the hardware. Most beginners spend their first month learning feeds and speeds, not fixing the machine.
Axes, Motion, and Tooling
A standard hobby CNC router moves on three axes: X (left/right), Y (front/back), and Z (up/down). That covers 90% of woodworking tasks — signs, joinery, inlays, flat-pack furniture. A 4th axis adds rotary motion for turning-style work or carving table legs; 5-axis machines exist but live in industrial shops.
Motion comes from either belts (cheap, slight stretch over long spans) or ball screws/lead screws (stiffer, more accurate, more expensive). The spindle matters most for cut quality:
- Trim routers (Makita RT0701-style, ~1–1.25 hp): standard on entry machines; loud, fine for wood.
- Water-cooled spindles (0.8–2.2 kW): quieter, more torque, better for long runs and harder materials.
- Bits: carbide end mills in 1/8″ and 1/4″ shanks dominate. Up-cut clears chips; down-cut leaves cleaner top edges; compression bits do both on plywood.
What Materials It Can Cut — and What It Costs to Own
Beyond solid wood and plywood, a CNC router handles MDF, HDPE, acrylic, soft aluminum (with care), foam, and Corian. What a product listing won’t tell you is the ongoing cost of ownership:
| Item | Typical spec / cost | Replacement interval |
|---|---|---|
| Carbide end mills (1/4″ up-cut) | $8–25 each | Every 10–40 hrs of cutting; dull bits burn wood and chatter |
| V-bits (60°/90°, for sign lettering) | $10–20 each | Months of hobby use; tips chip if fed too fast |
| Spoilboard (MDF, 3/4″) | $15–30 per sheet | Resurface every few projects; replace 1–3×/year |
| Dust collection | $100–400 (shop vac + dust shoe) | Ongoing; MDF dust is the real cleanup burden |
| Belts / v-wheels | $10–40 per set | 6–18 months; first parts to wear on belt-driven machines |
| Software (VCarve Desktop, etc.) | $0–350 one-time | Free options exist (Easel basic, Kiri:Moto, Carbide Create) |
Realistic accuracy on a well-tuned hobby machine is ±0.1–0.25 mm — plenty for joinery if you design in clearance, but not metalworking-tolerance.
What Beginners Actually Need: Choosing by Situation
The most common mistake is buying working area you don’t use. A 300×300 mm machine cuts full-size signs, coasters, and inlays; a 1000×1000 mm machine needs a dedicated bench and enclosure. Here’s how the decision actually breaks down:
| Your situation | Recommended type | Work area | Budget range |
|---|---|---|---|
| Curious hobbyist, signs & small decor, garage shelf space | Compact belt-drive (3018-class or similar) | ~300×180–400×300 mm | $150–400 |
| Maker selling signs/inlays, weekend use, workbench available | Mid-size gantry (e.g., X-Carve-, Shapeoko-, or Onefinity-class entry) | ~750×750 mm | $1,200–2,500 |
| Cabinet/panel work, plywood furniture, daily use | Rigid 4×4 ft machine with water-cooled spindle | ~1200×1200 mm+ | $3,000–7,000 |
| Production shop, nested-sheet cabinetry | Industrial 4×8 ft with vacuum table & ATC | 1220×2440 mm | $15,000+ |
A few realities listings gloss over:
- Rigidity beats size. A stiff small machine cuts cleaner than a flimsy big one. Aluminum extrusion frames flex above ~1 m spans unless braced.
- Dust is a workshop health issue. A dust shoe plus shop vacuum isn’t optional — fine wood dust (especially MDF) is a respiratory hazard; use extraction and a respirator during long sessions.
- Workholding causes most beginner failures. Clamps in the toolpath or a workpiece that shifts mid-cut ruin more projects than bad G-code. Use a spoilboard with threaded inserts or tape-and-CA-glue.
- Time is the hidden cost. A 30-minute carve is really 10 min setup + 30 min cut + 10 min cleanup per piece — factor that into whether batch production makes sense for you.
FAQ
Does “CNC machined” mean better quality than handmade?
It means consistent, not automatically better. CNC parts are dimensionally identical to ~0.1 mm, which matters for joinery and multi-part assemblies. Surface finish still depends on bit sharpness, feeds, and wood species — a poorly configured CNC leaves worse edges than a skilled hand.
Can a CNC router cut metal?
Hobby machines handle aluminum and brass slowly with shallow passes and proper bits; steel is generally beyond them due to rigidity limits. Cutting metal also requires chip management and often lubrication.
How hard is the software to learn?
Basic 2.5D work (signs, profiles, pockets) is learnable in a weekend with tools like Easel or Carbide Create. Full 3D carving and multi-sided setups take weeks of practice. Expect your first five projects to be learning exercises.
Do I need a computer permanently connected?
Depends on the controller. GRBL-based machines stream G-code over USB from a laptop; machines with offline controllers (e.g., those using a pendant or SD card) run standalone. Many hobbyists repurpose an old laptop as a dedicated sender.